Exclusive Patented Web Structure
Planar Universal Galvo with Dual-Axis Oscillation
X-Y Axis Bidirectional Oscillation
Supports circular, diamond and figure-eight oscillation patterns
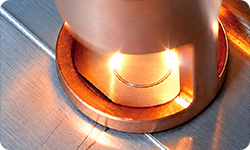
Reinforcement Rib Welding
Meets the load-bearing and safety requirements of structural parts
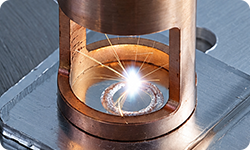
New Energy Battery Welding
Reduces the heat-affected zone and prevents cell burn-through
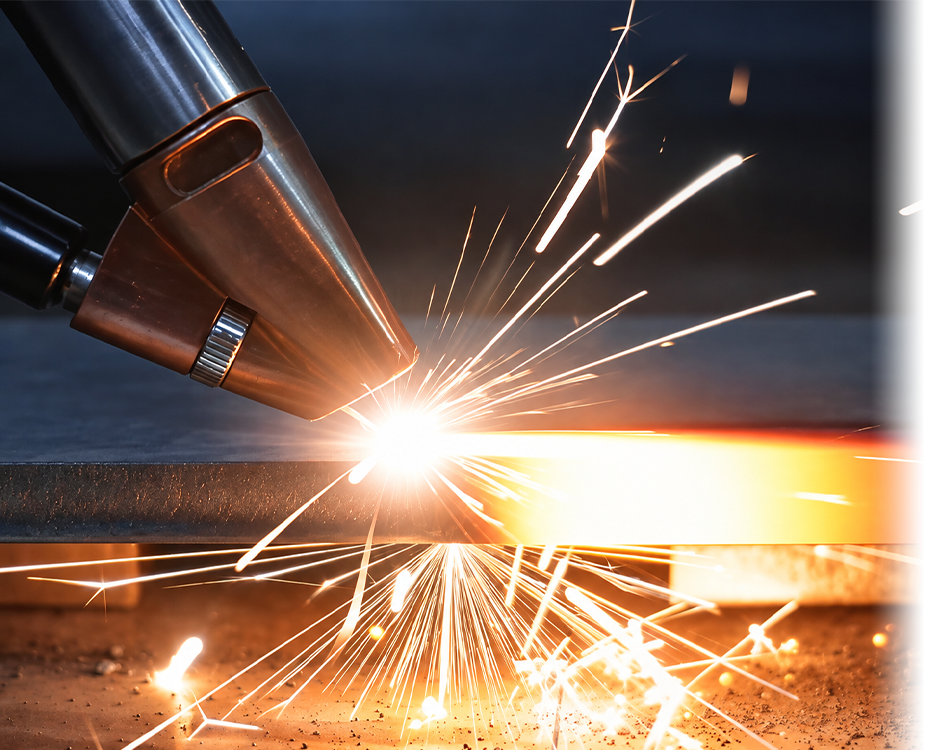
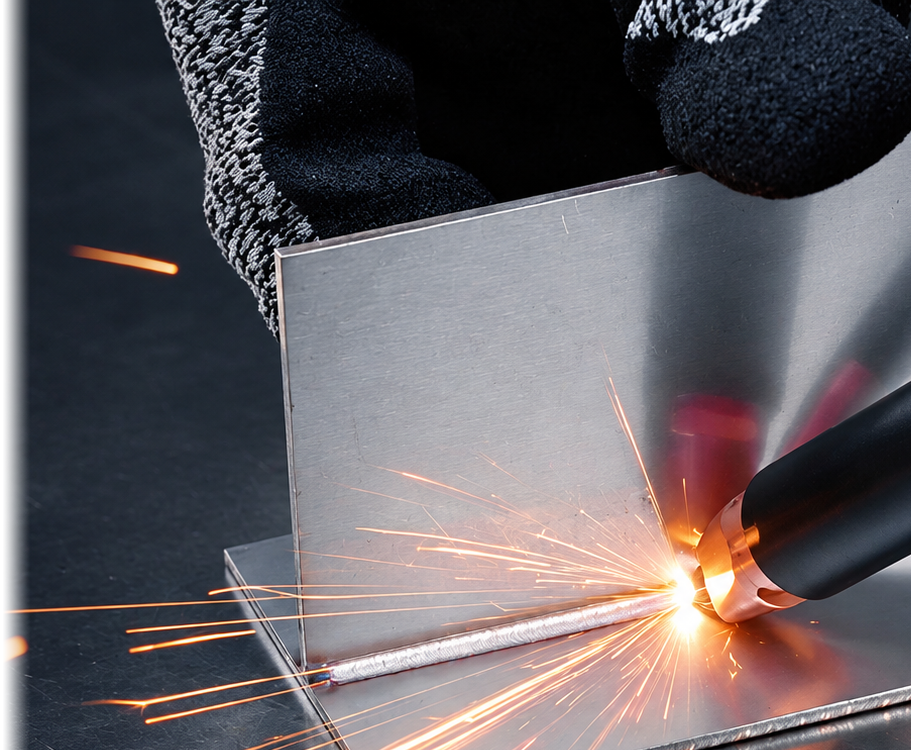
Deeper Penetration, Wider Welds
Handle Advanced Welding Applications with Ease
Eliminates insufficient penetration and lack of fusion on thick plates. In the upgraded D mode, penetration increases substantially, up to 6.0 mm. Built for deep penetration, wide weld seams and wide fillet welds, especially applications requiring build-up and high-speed welding.
30% deeper penetration | 22% higher maximum welding speed | Lower energy consumption (higher electro-optical conversion efficiency).
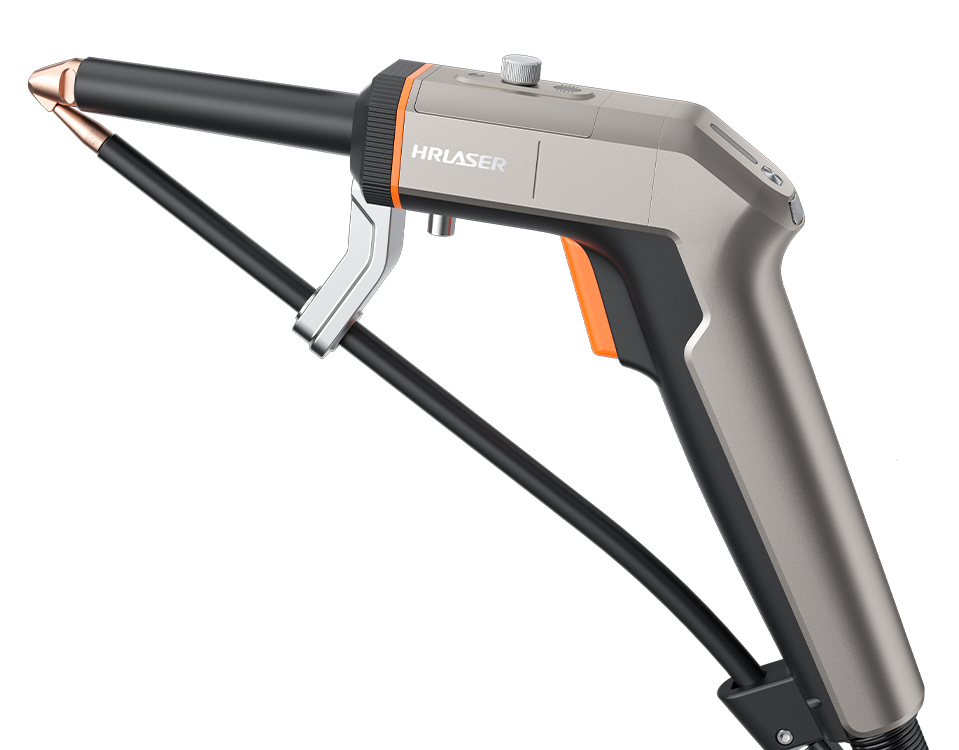
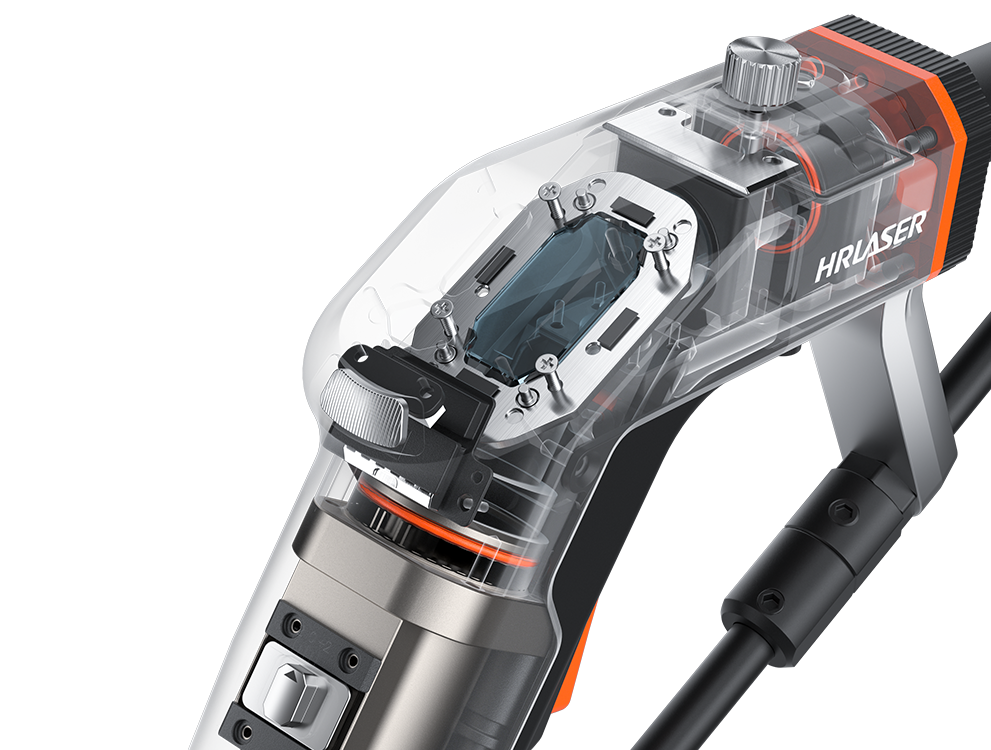
Ultra-Lightweight 380g Welding Torch
Less Effort, Greater Drop Resistance, Easier to Use
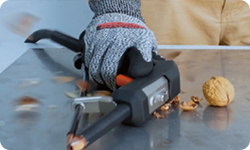
6–15× Improved Drop Resistance
Proprietary web structure with a re-engineered lever arm
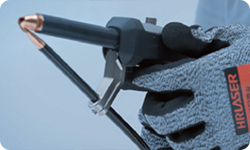
Proprietary Handle-Button Focus Adjustment
Adjust focus inside the torch without changing copper nozzles
More Convenient On-Torch Interaction
Multiple integrated high-frequency buttons on the torch, no need to walk back to the machine
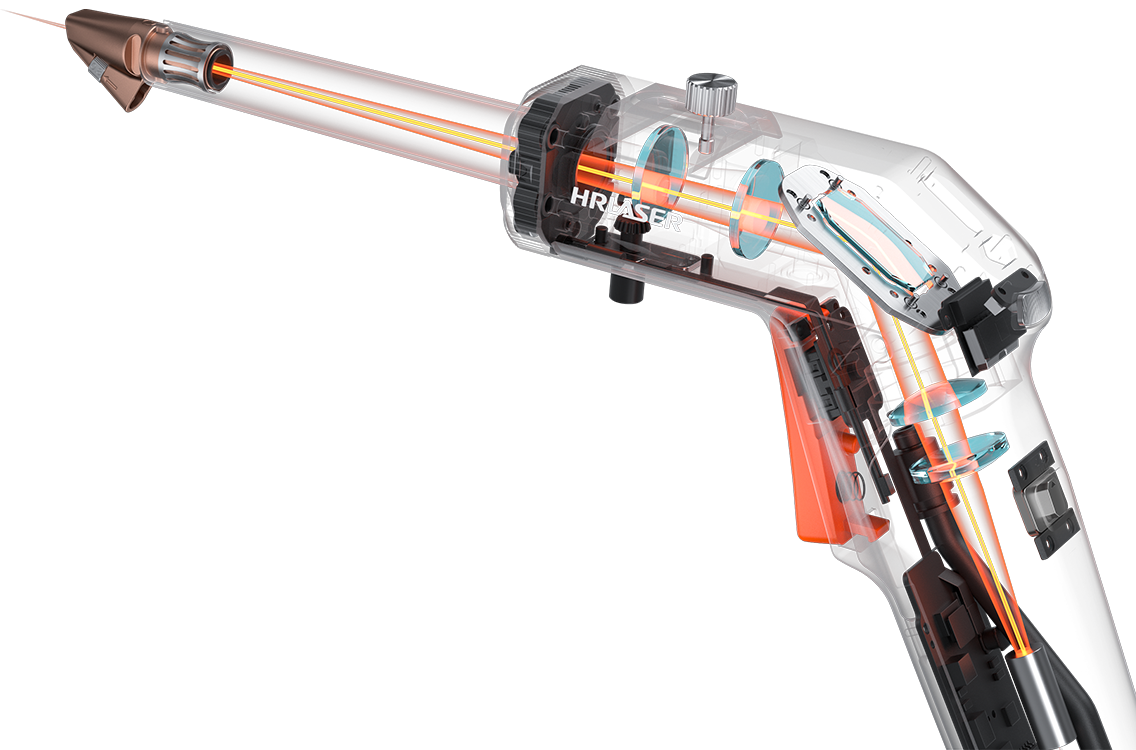
Proprietary Integrated Telecentric Optical Path
Breaking Industry Barriers to Overcome Hot-Dip Galvanized Steel Welding
For hot-dip galvanized sheet with a 50–150 μm zinc coating, this design solves the industry problems of weld spatter explosion, heavy spatter and lens burn-through. A reconstructed optical path and dual protective-lens shielding deliver the highest level of lens protection.
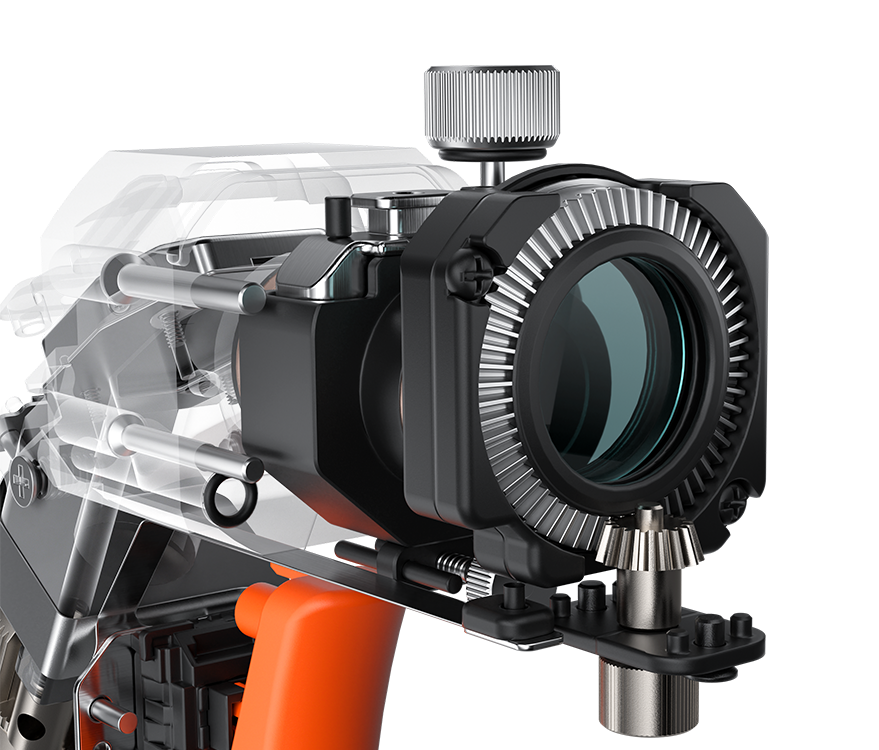
Proprietary Seven-Position Rotating Protective Lens
One Lens, Up to Seven Uses
Temperature Monitoring & Alarm — shifting from passive replacement to proactive alerts, so the lens is changed before damage occurs.
Triple-Layer Physical Spatter Shielding — a small-diameter nozzle blocks spatter at the source, with two internal spatter-blocking rings.
Proprietary Gas-Saving Brightening Technology
Gas Consumption Reduced from 15 L/min to 8 L/min
An industry-leading energy-saving configuration cuts shielding gas consumption by nearly half. Combined with an ultra-long-life protective lens and a low-loss machine design, it substantially reduces electricity and consumable costs for a clear cost advantage.
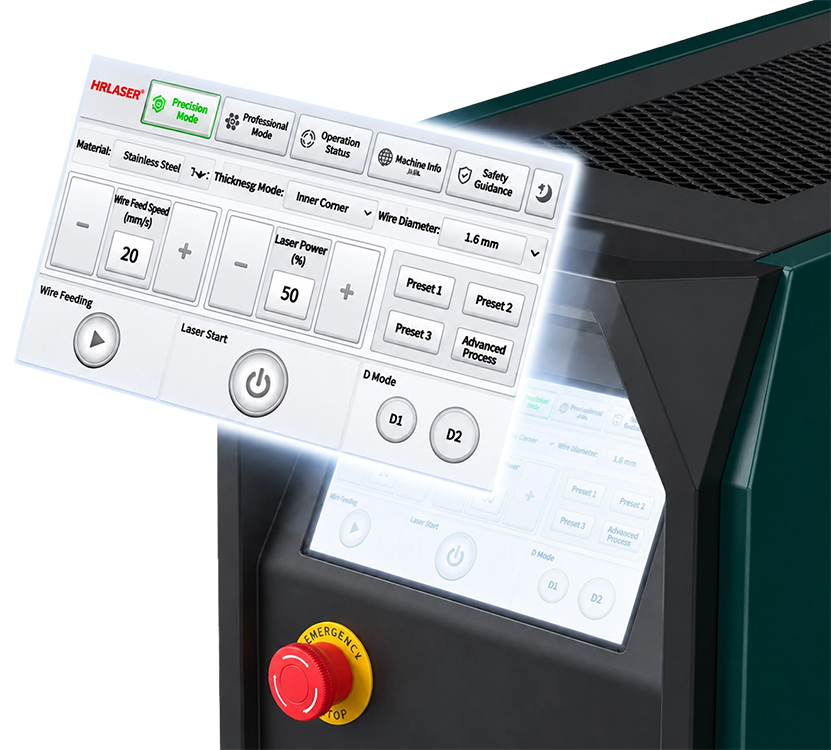
1,500+ Welding Process Presets
Easily Select the Optimal Mode
Material thickness selection refined from 1 mm to 0.1 mm for more precise process matching. The built-in library has grown from 538 parameter sets to more than 1,500 process presets, significantly improving welding accuracy and ensuring every weld meets the optimal standard.
* The exact process library depends on the model; refer to the actual product.
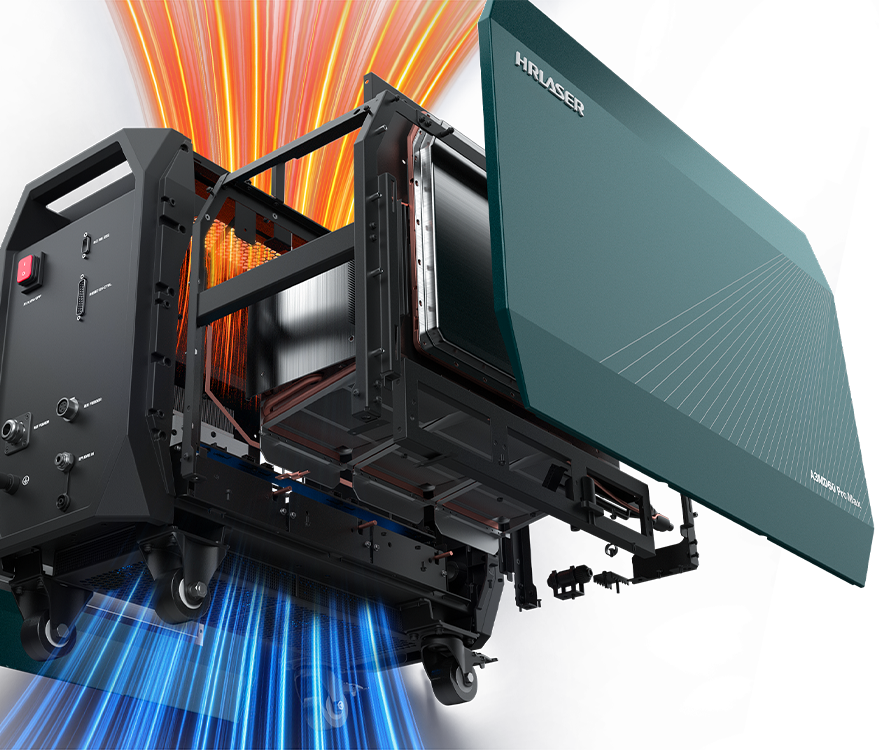
Enhanced Cooling, Reduced Noise
Validated in the Industry's Only Laser Welding Noise Test Laboratory
Refined through thousands of design iterations. A stacked-tooth heat dissipation structure with thinner, lighter teeth channels heat directly from the source to the aluminium fins; 6–8 high-performance 92 × 38 mm low-noise fans and a high-performance copper tube array provide efficient heat conduction and dissipation.
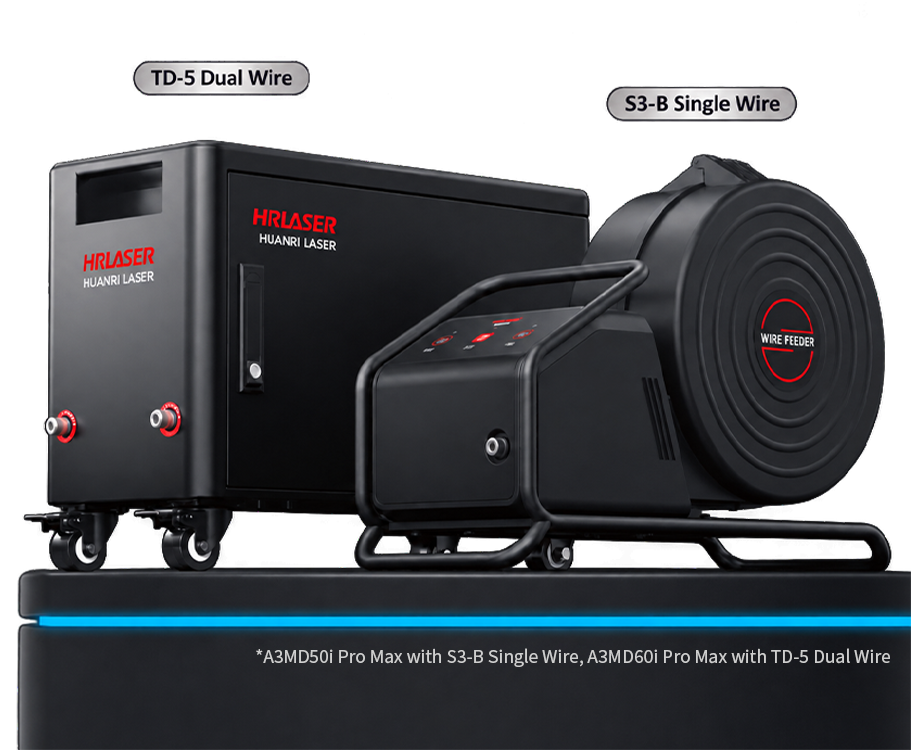
Dual-Drive Stepper Wire Feeding
100% Automatic Wire Cutting
Supports dual-wire feeding by default and remains compatible with single-wire feeding. An all-new dual-drive stepper motor delivers stronger wire feeding with 100% automatic wire cutting. The fully enclosed design protects the internal wire-feeding mechanism for greater safety and reliability, while the spool and feed assembly share a common centreline to reduce friction and keep feeding smooth.
Proprietary 4-in-1 feed wheel covers 0.8 / 1.0 / 1.2 / 1.6 mm wire, eliminating wheel changes and downtime; the 4-in-1 variable-diameter nozzle switches between four wire sizes by rotation with a fixed feed angle.
* The 4-in-1 feed wheel is an optional accessory.